Skip to content
Request a quote

High-purity pharmaceutical-grade ethanol for your business needs

Looking for a reliable supplier of pharmaceutical-grade ethanol? Nedstar provides high-purity ethyl alcohol for the pharmaceutical industry, healthcare products, disinfectants, and other applications requiring strict quality standards.

Our medical grade ethanol is sourced from trusted producers and supplied according to internationally recognised pharmacopoeial specifications, including USP, Ph. Eur., BP, and JP. Benefit from consistent quality, batch-specific documentation, flexible bulk packaging, and reliable international deliveries.

Nedstar Pharma
fusel oil nedstar

What is pharmaceutical grade ethanol?

Pharmaceutical-grade ethanol is high-purity ethyl alcohol (C₂H₅OH) produced and tested according to specifications established for pharmaceutical applications. It is a colourless, volatile liquid used as a solvent, preservative, processing aid, and active ingredient in selected medical formulations.

It is generally supplied without toxic denaturants for medicines and formulations intended for human use. However, pharmaceutical-grade pure alcohol does not mean that concentrated ethanol is safe for direct human consumption.

At Nedstar, we offer pharmaceutical ethanol at 96% ABV and 99.9% ABV, produced primarily from non-GMO sugarcane. Our products support manufacturers that require reliable quality, appropriate documentation, and compliance with applicable pharmaceutical standards.

Why choose Nedstar as your pharmaceutical ethanol supplier

Reliable international sourcing

Nedstar connects pharmaceutical manufacturers with an established network of certified alcohol producers. Our sourcing expertise helps customers secure high-purity ethanol for medicines, antiseptics, extraction processes, and other healthcare applications.

Consistent purity and specifications

Nedstar works with GMP-compliant production facilities and supports batch-specific Certificates of Analysis (CoAs), helping customers verify that supplied alcohol meets the specifications required for their intended applications.

Our product documentation supports quality assurance, regulatory reviews, and supply chain traceability.

Flexible bulk supply and logistics

Whether you need 96% ethyl alcohol for medicinal formulations or 99.9% anhydrous ethanol for moisture-sensitive processes, Nedstar helps arrange reliable supply according to your production requirements.

Our pharmaceutical-grade ethyl alcohol portfolio

Nedstar offers a range of ethanol products for pharmaceutical and healthcare manufacturing. Product suitability depends on the required pharmacopoeial grade, intended application, and individual specifications.

Extra neutral alcohol (ENA 96%)

High-purity ethanol suitable for selected pharmaceutical formulations, tinctures, extraction processes, and disinfectant production. Available in conventional and certified organic grades.

Anhydrous ethanol 99.9%

Highly concentrated ethanol with a purity of at least 99.5% and minimal water content, designed for applications requiring low moisture levels and controlled solvent properties.

Organic pharmaceutical alcohol

 Ethanol produced from certified organic raw materials, suitable for manufacturers with specific sourcing preferences and traceability requirements, subject to the required pharmaceutical specifications. 

REN Alcohol

Rectified ethanol of natural origin, offering consistent composition for suitable pharmaceutical, chemical, and technical manufacturing applications.

How is pharmaceutical grade ethanol produced?

The production of pharmaceutical grade ethanol involves several key stages, including fermentation, distillation, dehydration, and quality testing, to achieve the required purity and pharmaceutical standards.

1-Aug-08-2025-07-53-18-0394-AM

Raw material processing

Ethanol can be produced from agricultural raw materials containing fermentable sugars or starches, including sugarcane, sugar beet, maize, and wheat.

Starch-based feedstocks require additional processing to convert complex carbohydrates into sugars suitable for fermentation.

Fermentation-derived ethanol is also referred to as bioethanol, although pharmaceutical applications require additional purification and quality testing.

2-3

Fermentation

During fermentation, sugars are fermented by yeast, producing ethanol and carbon dioxide through a biochemical process.

Fermentation commonly produces alcohol concentrations of approximately 10–15%, depending on the raw materials, yeast strain, and operating conditions.

Ethanol can also be synthesised through the hydration of ethene using a phosphoric acid catalyst. However, Nedstar's pharmaceutical ethanol is primarily sourced from agricultural feedstocks.

3-3

Distillation and dehydration

Distillation separates ethanol from the fermentation mixture in a controlled manner, increasing its concentration by exploiting differences in volatility.

Conventional distillation can concentrate ethanol to approximately 95–96%, while additional dehydration processes are used to produce anhydrous ethanol with very low water content.


4-Aug-08-2025-07-53-17-8410-AM

Purification and quality testing

Further purification removes unwanted impurities and other substances, ensuring pharmaceutical ethanol meets the required purity specifications.

Quality testing includes verifying ethanol concentration, water content, chemical properties, and impurity limits, including methanol.

Batch-specific Certificates of Analysis confirm compliance with applicable pharmacopoeial standards and support consistent product quality.
 

Applications

What is pharmaceutical grade ethanol used for?

denaturantes nedstar chemicals
Pharmaceutical formulations and medicines
  • Dissolving selected active pharmaceutical ingredients (APIs) and excipients
  • Acting as a carrier solvent in oral solutions, tinctures, and topical preparations
  • Supporting the manufacture of syrups and other liquid medicines
  • Serving as a volatile processing aid during wet granulation in tablet production
  • Functioning as a preservative or stabilising ingredient in suitable formulations
Nedstar-hand-sanitizers
Antiseptics, disinfectants, and hygiene products
  • Manufacturing alcohol-based hand sanitisers and disinfectant gels
  • Producing antiseptic solutions for skin disinfection in approved applications
  • Formulating suitable disinfectants for healthcare environments
  • Supporting the preparation of iodine tinctures and other topical antiseptics
  • Cleaning compatible surfaces and equipment under validated procedures
pharmaceutical-extraction-research
Pharmaceutical extraction and research
  • Extracting active phytochemicals from medicinal plants
  • Preparing botanical extracts and herbal medicines
  • Supporting solvent-based separation and purification processes
  • Serving as a reaction medium in selected chemical synthesis procedures
  • Preparing samples and solutions for pharmaceutical research
  • Supporting molecular biology research and laboratory sample preparation
  • Removing compatible adhesive residues from laboratory equipment
  • Cleaning compatible laboratory glassware and instruments
Perfume_Nedstar
Cosmetics and personal care products
  • Dissolving fragrances and other formulation ingredients
  • Acting as a carrier in perfumes and cosmetic solutions
  • Supporting the extraction of selected botanical compounds
  • Formulating suitable cleansing and hygiene products
  • Providing rapid evaporation in certain topical formulations
nedstar-cosmetics-organic-lotion
Specialised medical applications
  • Supporting the manufacture of certain medical and healthcare products
  • Serving as an ingredient in approved topical preparations
  • Acting as a therapeutic agent in specific procedures, such as percutaneous ethanol injection, when supplied and administered under appropriate medical standards
Choosing the right pharmaceutical grade ethanol

Selecting pharmaceutical ethanol requires careful consideration of its intended use, chemical composition, regulatory requirements, and supply documentation.

Important purchasing factors include:

  • Pharmacopoeial compliance: Confirm whether USP, Ph. Eur., BP, JP, or another recognised standard applies.
  • Ethanol concentration: Choose a suitable assay and water content for the manufacturing process.
  • Impurity limits: Verify methanol, organic impurities, and other relevant substances against the required specifications.
  • Denaturation: Ensure the formulation contains only additives permitted for its intended application.
  • Manufacturing standards: Review GMP requirements and supplier quality documentation.
  • Packaging: Select suitable containers that help prevent contamination during storage and transportation.
  • Traceability: Request batch-specific Certificates of Analysis and supporting documentation.

Nedstar helps procurement teams evaluate these requirements and source pharmaceutical ethanol aligned with their manufacturing needs.

nedstar-pharma

Key attributes of pharmaceutical-grade ethanol


adding-value

High purity and controlled impurities

Pharmaceutical ethanol is produced and tested against defined quality specifications. Controlled impurity levels help reduce the risk of unwanted chemical interactions, contamination, and potential adverse effects on patients.

Uncontrolled impurities can affect drug stability, reduce potency, and alter the absorption of active ingredients, making strict quality control essential for pharmaceutical applications.


bottom-line

Strong solvency and formulation versatility

Ethyl alcohol dissolves many organic compounds, including certain resins, and mixes readily with water, making it a versatile solvent for medicines, extraction processes, and topical preparations.

Its solvent properties support consistent ingredient distribution and formulation performance.


biochemicals icon

Antimicrobial properties

At suitable concentrations, ethanol disrupts microbial membranes and denatures proteins, helping eliminate susceptible bacteria in approved antiseptic and disinfectant formulations.

Its effectiveness depends on factors such as alcohol concentration, contact time, and the microorganisms involved.


dynamic

Reliable quality and traceability

Consistent specifications and batch documentation are essential for pharmaceutical manufacturing.

Nedstar supports customers with product information and quality documentation to help maintain traceability throughout procurement and production.

 

Pharmaceutical-grade ethanol vs. industrial ethanol: What's the difference?

Although pharmaceutical and industrial ethanol contain the same chemical compound, their specifications, impurity controls, and intended applications can differ significantly.

Property

Primary applications
Purity requirements
Impurity controls
Denaturation
Documentation

Pharmaceutical grade ethanol

Medicines, healthcare, pharmaceutical processing
Defined by applicable pharmaceutical specifications
Strict limits for relevant contaminants
Generally undenatured for medicinal formulations
Pharmacopoeial testing, CoAs, and applicable GMP records

Industrial ethanol

Chemical manufacturing, cleaning, fuels, and technical processes
Determined by technical or industrial requirements
Vary according to industrial grade and application
May be denatured or undenatured
Technical specifications, CoAs, and safety documentation as required

Can denatured ethanol be pharmaceutical grade?

Denatured ethanol contains additives that make it unsuitable for drinking. These may include substances such as isopropyl alcohol, methyl ethyl ketone, or other approved denaturants. Such formulations can be used in certain external-use products, provided their composition complies with the applicable requirements. However, denatured ethanol is generally unsuitable for medicines intended for ingestion.

Nedstar offers information on different denaturants to help customers understand their properties and technical applications.

Pharmacopoeia standards for pharmaceutical-grade ethanol

Pharmaceutical ethanol must meet the requirements of the relevant pharmacopoeial standards and regulatory guidelines for its intended market.


USP-grade

The United States Pharmacopeia (USP) establishes quality specifications for pharmaceutical substances, including relevant ethanol grades. These standards address identity, assay, and applicable impurity limits. 

EP-grade

The European Pharmacopoeia (Ph. Eur.) provides recognised quality standards for pharmaceutical substances used across European markets. Its ethanol monographs define relevant testing requirements and acceptance criteria. 

BP-grade

The British Pharmacopoeia (BP) establishes official specifications for medicinal substances and pharmaceutical preparations in the United Kingdom. 

JP-grade

The Japanese Pharmacopoeia (JP) defines quality requirements for pharmaceutical substances intended for the Japanese market. 


What
makes
Nedstar
different?

reach-darkgreen
Reach

 REACH provides a framework for gathering and evaluating information on the properties, uses, and potential risks of various chemicals. 

non-gmo-darkgreen
GMO-free

 GMO-free certification options allow customers to source ethanol that meets their requirements for non-genetically modified raw materials and traceable origins. 

usda-organic-darkgreen
USDA-NOP

Nedstar offers USDA-certified organic products that comply with National Organic Program standards, helping customers source certified organic raw materials. 

eu-organic-darkgreen
EU Organic

 EU Organic certification helps ensure that eligible agricultural products meet European organic standards, supporting traceability, regulatory compliance, and accurate product labelling. 

Nedstar packaging options for bulk pharmaceutical ethanol

Appropriate packaging helps protect pharmaceutical ethanol from contamination and supports safe international transportation. Nedstar offers flexible packaging options for customers sourcing medical grade ethanol in bulk.

1,000 Litres
IBC tote

IBC Nedstar

Mid-sized shipments: our stackable IBC totes provide an efficient and reliable solution for transporting fusel alcohols.

25,000 Litres
ISO container

ISO tank Nedstar

Bulk international shipments: ISO containers offer a secure and efficient option for transporting fusel oils across global supply chains. 

35,000 Litres
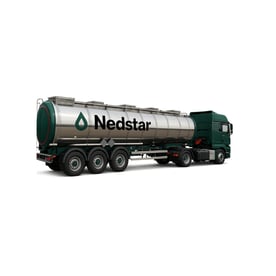
Tanktruck

Tank truck Nedstar

Large-volume deliveries: tank trucks provide an efficient solution for regional transport of fusel alcohols. 

Frequently Asked Questions